
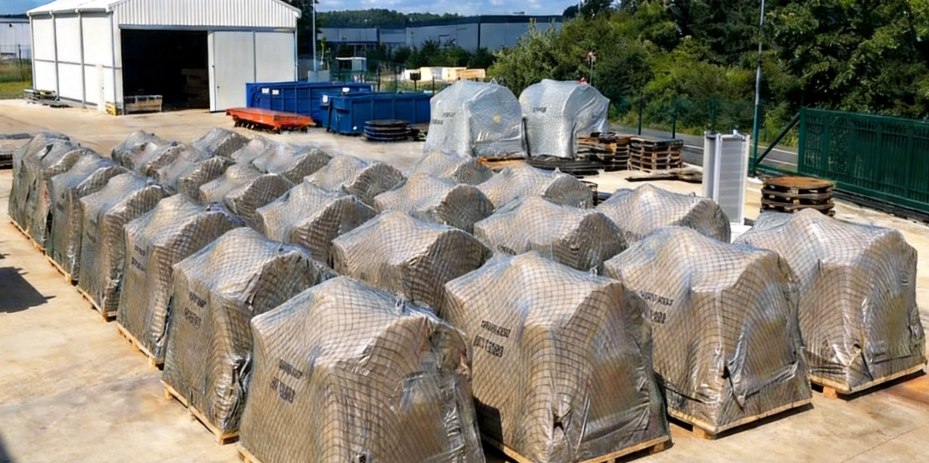
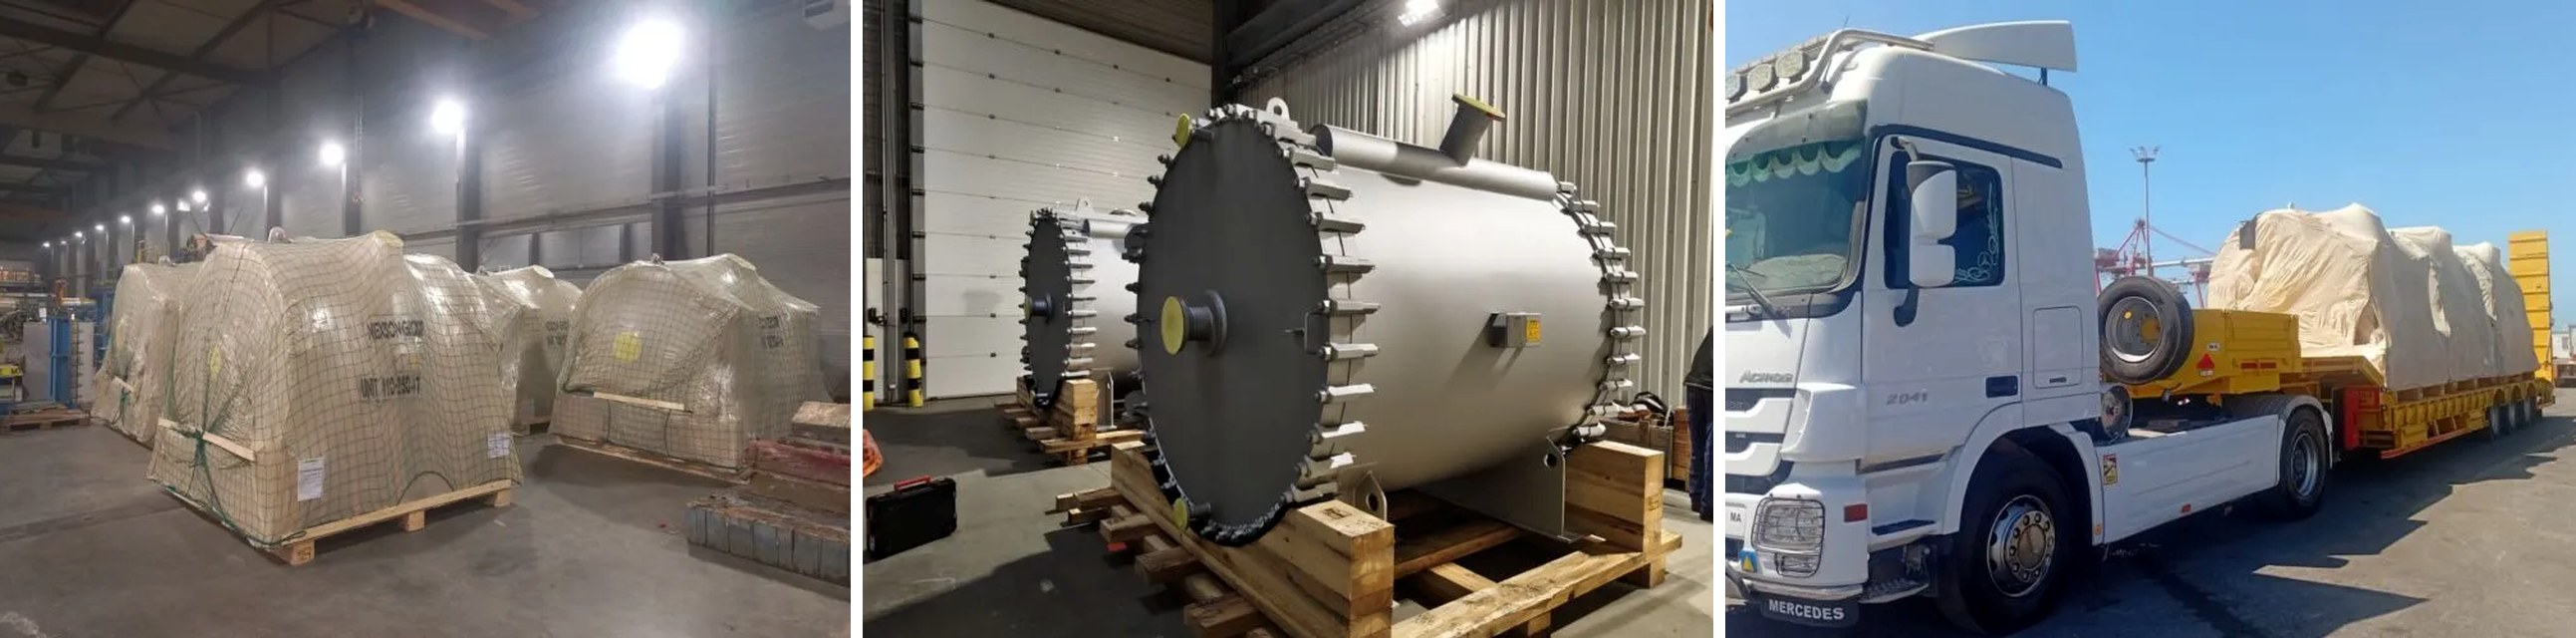
Nexson Group has completed delivery of 22 custom-built super duplex spiral plate heat exchangers. Designed for the demanding duties of phosphate rock mining and phosphate chemicals, they handle the complex heat transfer and corrosive media of the industry, reflecting the company’s capability in custom design and manufacturing of industrial heat exchange equipment.
The challenge of a severe duty
In phosphate chemical production, cooling phosphoric acid with seawater is one of the more severe heat transfer applications. The process presents a two-sided corrosion duty: the two sides of the equipment contact corrosive phosphoric acid on one side and high-salinity seawater on the other, in a complex corrosive environment over the long term, placing high demands on both material reliability and structural stability.
Material selection directly affects the operating safety, service life and operating economy of the whole production system. Conventional standard heat exchange equipment has limited corrosion and fouling resistance and cannot adapt to this kind of extreme duty: it fails readily in long-term operation, raises maintenance cost, and struggles to meet the requirements of continuous industrial production.
Super duplex steel plus spiral structure
To address the corrosion, scaling and heat transfer stability issues of seawater-cooled phosphoric acid, Nexson Group completed a purpose-built scheme optimisation against the duty parameters, improving duty adaptation through material upgrade and structural optimisation.
The units are built in super duplex stainless steel, which offers strong resistance to pitting and crevice corrosion under combined chloride and acid conditions. It suits the corrosive environment of seawater-cooled phosphoric acid, keeps equipment running steadily over the long term and extends service life.
The units use the single-channel structure specific to spiral plate heat exchangers, which produces a stable self-cleaning effect in operation — reducing fouling build-up, avoiding channel blockage and maintaining stable heat transfer efficiency. This design cuts maintenance frequency, reduces system downtime, and lowers overall project operating cost.
Project highlights
Delivery scale: 22 high-performance spiral plate heat exchangers, matched to a large continuous industrial production system.
Core material: super duplex stainless steel, suited to highly corrosive, high-salinity complex duties.
Application: the core process of seawater cooling of phosphoric acid in phosphate chemicals.
Benefits: strong corrosion and fouling resistance, long-term efficient operation, lower operating and maintenance cost, balancing production safety with economic practicality.
Heat exchange technology capability
The smooth delivery of this project verifies Nexson Group’s ability to carry technology through the full chain — scheme design, precision manufacturing and duty adaptation for industrial heat exchange equipment — and to supply stable, reliable and efficient heat exchange equipment for harsh duties in the chemical and mining industries, supporting the stable operation of production systems.
Going forward, Nexson Group will keep focusing on iteration of industrial heat exchange technology and process optimisation, and steadily raise its capability in custom supply of high-end industrial equipment.